The process of welding armor steel is a complex process not only due to high percentage of carbon in the base metal, but also because of possible welding faults, appearing in the weld metal zone in the form of cracks and pores.
Austenitic filler material is traditionally used for welding armor steels, thus avoiding the negative effect of hydrogen content due to slow diffusion towards the sensitive fusion line.
For heavy structural engineering such as armored military vehicles, which are frequently under the effect of impact and dynamic load,
it is important to know the dynamic properties of the most sensitive area of welded joints, the weld metal zone.
Laser welding of high hardness Armor steel
Laser Welding of ARMOX Steel
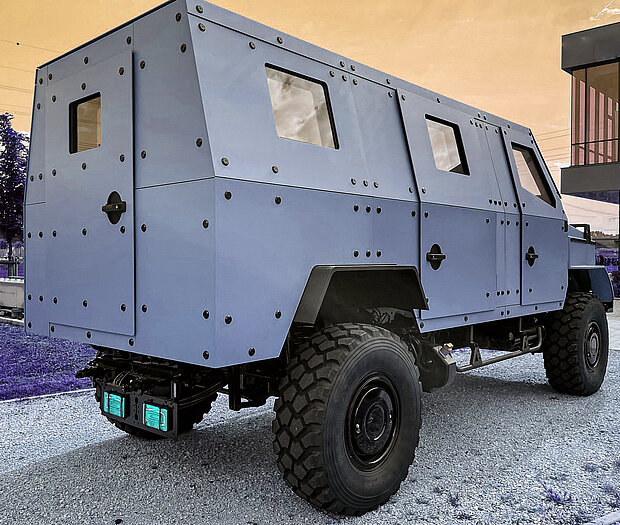
Armored vehicles must provide high ballistic protection, and on the other hand, they must have the lowest possible weight to ensure high mobility even in very difficult terrain and environments. The basic structural material for such vehicles is steel because it is susceptible to plastic processing, joined via welding, and facilitates the shaping of functional properties in a wide range as a result of heat treatment. Steels that provide good ballistic properties are usually ultra-high strength (UHS) steels processed by quenching and tempering (Q&T). High mechanical properties are provided by martensitic microstructure. However, due to subsequent tempering, the ductility and toughness is increased, providing better impact energy absorption which is crucial for ballistic performance. Many researchers involved in testing the ballistic characteristic of armor plates made of different grades of armor steel indicate that the higher the hardness of the steel obtained as a result of tempering, the higher the ballistic resistance. Therefore, tempering takes place at a relatively low temperature, retaining high hardness and thus high ballistic performance.
The most commonly used joining methods of the armor steel components are gas metal arc welding (GMA) and submerged arc welding (SAW). All of the mentioned methods usually utilize austenitic type wire as the additional material because the weldability of the armor grade steel is limited due its high carbon equivalent, high hardness, and thus tendency for cold cracking. However, the use of a plastic austenitic deposit leads to a significant reduction in the ballistic performance of welded joints, Moreover, even the plastic and relatively soft austenitic deposit does not completely solve the problem of hydrogen-induced cracking (HIC) in the heat-affected zone (HAZ) of the welded joints of armor steel [
Welding Processes and Ballistic Performance of Armor Steel
Welding of armour steel demands a careful balance between metallurgical integrity and protective performance. Common fusion processes—from Shielded Metal Arc Welding (SMAW) and Gas Metal Arc Welding (GMAW) to advanced Plasma Transferred Arc (PTA) and laser methods—must be tailored to high-hardness alloys that are susceptible to hydrogen-induced cracking and softening in the heat-affected zone (HAZ). Control of heat input, filler composition and cooling rates governs the evolution of microstructures such as tempered martensite and bainite, which in turn determine hardness, toughness and ballistic resistance. Optimised procedures aim to minimise weakened HAZ regions, preserve base-metal strength and ensure welds achieve comparable V50 limit velocities under projectile impact. Such refinements are critical for lightweight vehicle armour, structural retrofits and next-generation protective systems where global forces demand both resilience and weight efficiency.
Laser Welding, a method that has not yet been used industrially for the welding of armor steel, but providing a lot of benefits and gives the possibility of further optimization and development of welding technology of this grade of steel. Laser welding may be conducted as an autogenous process, without additional material, and thanks to efficient shielding of inert gas, the process can be considered as a low-hydrogen process. Moreover, the characteristic feature of laser welding is a narrow HAZ and a relatively low level of welding stresses, which in turn is beneficial to the reduction in the tendency for hydrogen-induced cracking.
The testings carried out so far in the field of laser welding of armor steel indicate that despite the low heat input of laser welding and rapid cooling, softening of HAZ occurs, which may be additionally beneficial in terms of the reduction in the tendency for hydrogen-induced cracking. It is also worth noting that currently available lasers with a power of several dozen kW allow for welding joints with a thickness over 30 mm in one pass.
Laser welding also shows some limitations. Since the laser beam is very a precise heat source, usually focused to a very small diameter, it requires high tolerance of edges preparation and positioning of the laser beam along the weld trajectory, in the case of butt joint welding. Moreover, in the case of autogenous welding, it is not possible to control the chemical composition of the weld metal, and weld undercuts are typical. These limitations make the application of laser welding on an industrial scale some more difficult in certain areas, but certainly not impossible!


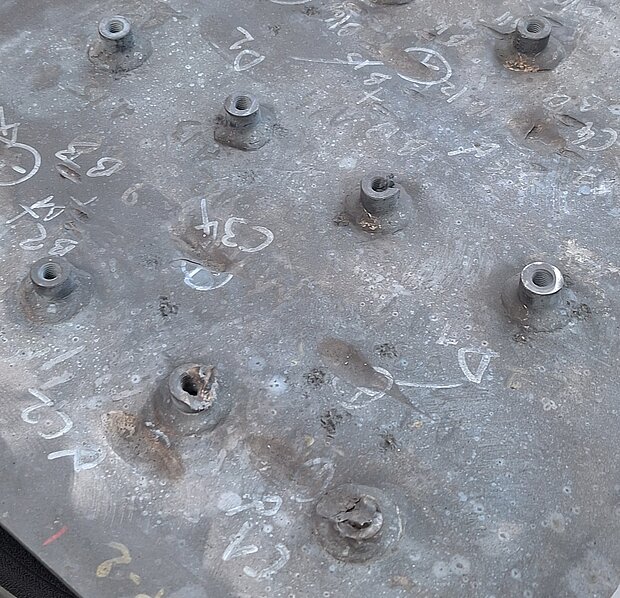
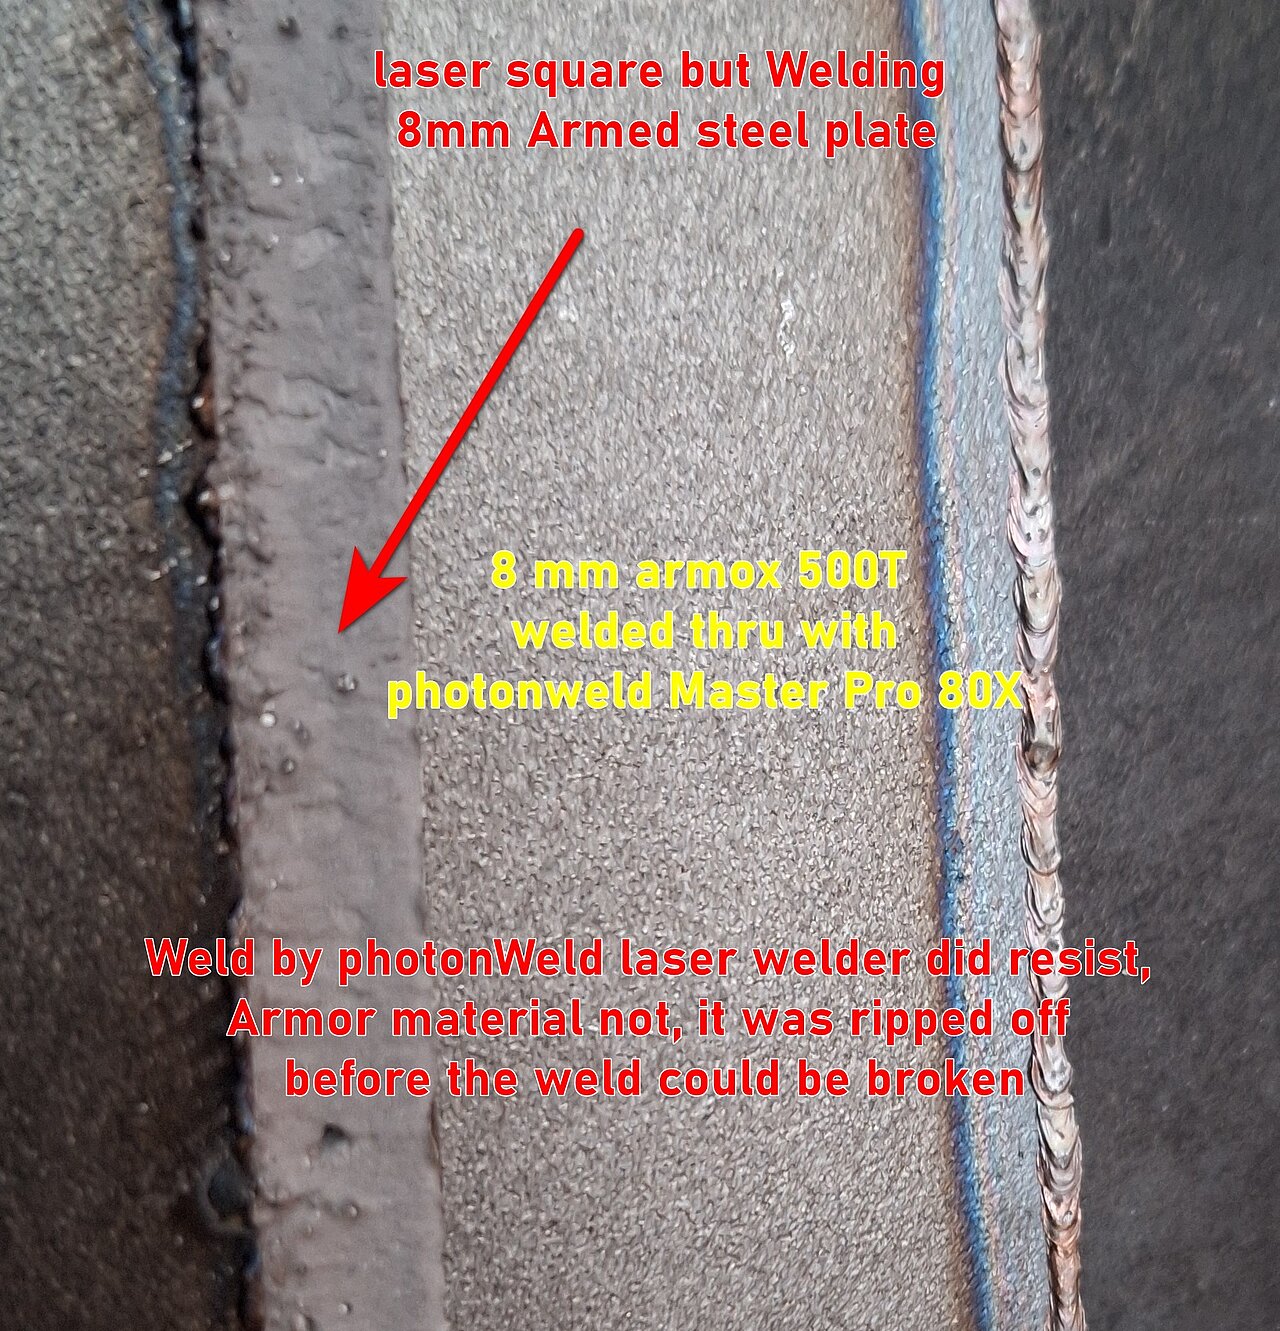
Schaft Ripped out of armor materia! The weld of 1,4 mm by handheld laser welder did resist, the material not.
Our laser welding by photonweld Master Pro X-80 is much stronger than the armor plate material itself!
Match over for hardened armor steel plates: our laserweld is stronger than the materiaal itself.
Look to the pictures of the welded parts ripped out from te material with intact weld